

Surface Treatment & Electroplating Solutions
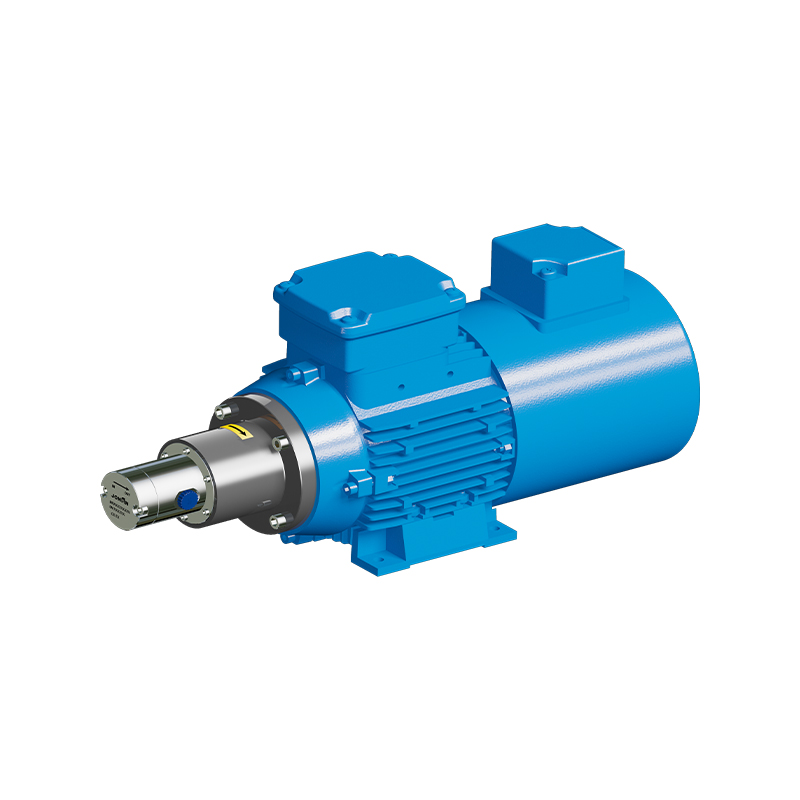
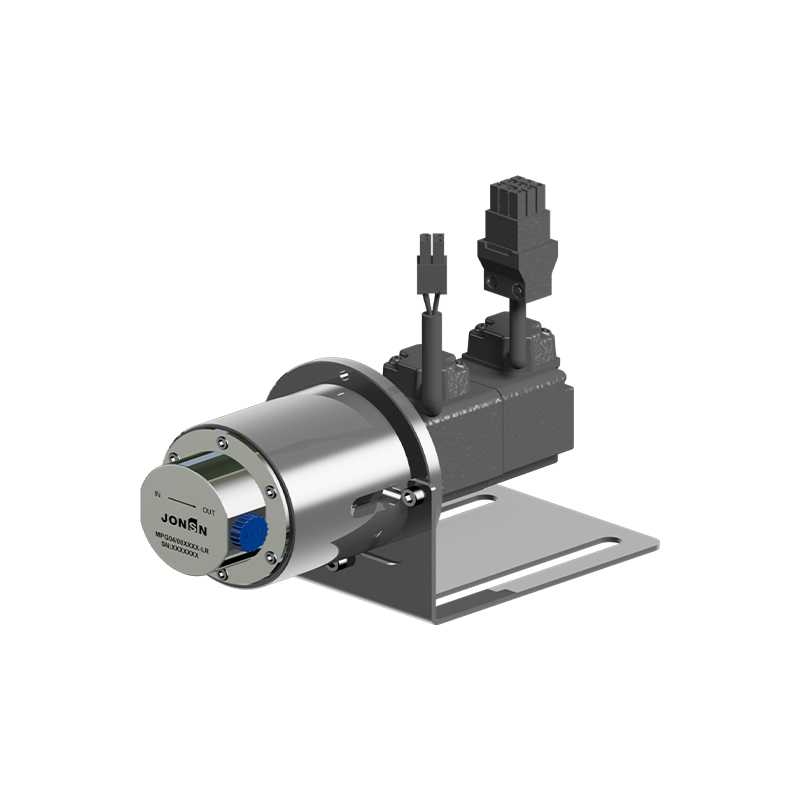
JONSN Micro Gear Pump Surface Treatment & Electroplating Solution
Surface treatment and electroplating are the "cosmetic specialists" of manufacturing—iMParting corrosion resistance, wear resistance, decorative and functional surfaces to metal and plastic components.
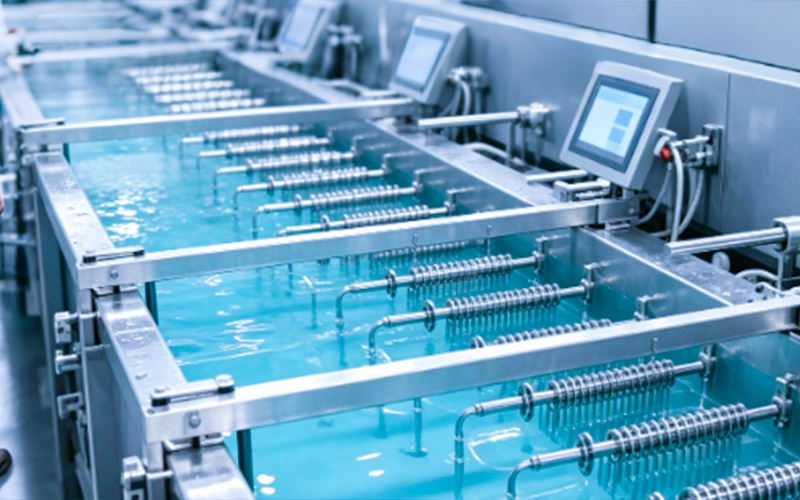
Manufacturing Cosmetics Specialist
Surface treatment and electroplating are the "cosmetic specialists" of manufacturing—iMParting corrosion resistance, wear resistance, decorative and functional surfaces to metal and plastic components.Full Process Scope
From automotive zinc-nickel alloy plating, electronic connector electroless nickel/gold plating, aerospace aluminum hard anodizing, car body electrophoretic coating, to fastener phosphating—every step relies on precise chemical delivery.Three Major Challenges
These processes share three major challenges: extreme corrosion from strong acids and alkalis (H2SO4, HCl, HNO3, NaOH); precise ppm-level replenishment of brighteners and additives; and complex conditions involving high temperatures, solid particles, and entrained bubbles.Category Text
Delivering an elite electroplating gear pump line, JONSN powers surface treatment chemical metering pump skids, Hastelloy plating solution pump units, and anodizing acid circulation pump systems.Six Core Industry Pain Points in Surface Treatment
Plating bath corrosion & anode sludge, electroless plating metal salt wastage, anodizing low-temperature acid contamination, phosphating crevice corrosion, pickling extreme acid attack, and brightener empirical dosing defects — each eroding coating quality, bath chemistry, and long-cycle plant economics.
Seven Detailed Surface Treatment & Electroplating Processes
Seven core surface treatment process solutions — plating bath circulation, electroless plating replenishment, anodizing & sealing, electrophoretic coating, phosphating/passivation, pickling, and smart brightener Ah-linked dosing — each mapped to recommended JONSN pump series (MRA / MRB / MPG / DP) with technical parameters and key adaptations.
Product Selection Quick Reference for Surface Treatment
Engineering selection matrix covering every surface treatment process — plating bath circulation, electroless plating, anodizing, electrophoretic coating, phosphating/passivation, pickling, and brightener replenishment — with media & operating conditions, recommended JONSN series, flow / displacement, and key adaptations.
| Process Step | Medium / Condition | Recommended Series | Flow / Displacement | Key Adaptation |
|---|---|---|---|---|
| Plating Bath Circulation | Ni/Cr/Zn Bath, 40–60°C, anode sludge | MRB/MRA Series | 0.1-4.8 L/min | 316L/C-276 Head, Large Clearance, Magnetic Seal |
| Electroless Plating | NiSO4/Cu/Au Conc., Ambient Temp | MPG Micro Series | 1–280 mL/min (40 μL/r) | Photoelectric Feedback, Viscosity Immunity, Zero Leaching |
| Anodizing & Sealing | 15–20% H2SO4, -5°C to 20°C, sealing agent | MRA (Bath) + MPG (Seal) | 0.1–2 L/min 1–280 mL/min | 316L Low-Temp H2SO4 Resistant, MPG Sealing Dosing |
| Electrophoretic Coating | Epoxy/Polyurethane Paint, 28–32°C | DP High-Viscosity Series | 0.2–100 cc/r | High Visc 50,000 MPa·s, Low Shear No Bubbles, PTFE |
| Phosphating & Passivation | H3PO4/HNO3/Zn Salts, 35–55°C | MRA × N Channels | 100–2,000 mL/min × N independent channels | Hastelloy C-276, Multi-Step Independent Metering |
| Pickling | HCl/H2SO4/HNO3+HF, Ambient-60°C | MRA Series (Hastelloy) | 100–2,000 mL/min | Hastelloy C-276, Magnetic Zero Leakage, Full Resistant |
| Brightener Replenishment | Thiourea/Alkyne Amines/Surfactants | MPG Micro Series | 1–280 mL/min (40 μL/r) | Ah Current Linked, Saves 15%–20% Chemicals |
Corrosion Resistance, Environmental Standards & Seven Core Engineering Values
Combined corrosion/environmental standards matrix and seven core engineering values — full metallurgy options, magnetic zero-leakage, chemical-proof seals, and 20,000h design life — turning JONSN into the single-source supplier for automated surface finishing lines across automotive, connector, and aerospace industries.
Full Metallurgy Options:
316L, Hastelloy C-276, and Titanium pump head options covering conventional pickling to extreme mixed acid corrosion.Full-Series Magnetic Zero-Leakage:
Full-series magnetic drive eliminates dynamic seals, preventing acid, alkali, solvent, and toxic solution leaks to meet environmental and occupational health standards.Chemical-Proof Seals:
PTFE, FFKM, and PEEK wetted flow path seals resistant to HCl, H2SO4, HNO3, HF, organic solvents, and strong oxidizers.20,000h Long Continuous Duty:
Design life >20,000 hours, matching long-cycle continuous duty on automated surface finishing lines.Surface Treatment Technical FAQ
How does an electroplating gear pump achieve 15%–20% chemical savings during brightener replenishment?
Conventional timed replenishment causes ±20%-30% dosing deviations, wasting costly brighteners (¥80–200/kg) and degrading coating luster. A JONSN electroplating gear pump (MPG series with 40 μL/r displacement) links with plating rectifiers/ammeters to automatically calculate and inject exact brightener volumes based on real-time Ampere-Hour (Ah) consumption. Its low-shear delivery prevents organic molecule degradation, saving 15%–20% on chemicals annually while locking uniform mirror gloss.
What microfluidic features make JONSN a premier surface treatment chemical metering pump for electroless plating?
In electroless nickel and gold plating (chloroauric acid >¥400/g), cavitation in acidic concentrates causes ±5% dosing errors, reducing plating speed by 20%–30%. A JONSN surface treatment chemical metering pump (MPG series) utilizes Mazak 5-axis carved PEEK gears and nanostructural Zirconia ceramic shafts. Paired with online photoelectric sensor feedback, it tracks metal ion decay with deviation <±1%, eliminating metal ion leaching and precious metal wastage.
Why is JONSN Hastelloy plating solution pump technology superior for severe hydrochloric and mixed acid pickling?
Pickling baths use 37% concentrated HCl, 98% sulfuric acid, and HNO3+HF mixed acids that cause pitting and crack ordinary metal pumps within 2–4 months. Every JONSN Hastelloy plating solution pump (MRA series) is CNC-carved from solid Hastelloy C-276 blocks paired with PTFE/FFKM seals rated >200°C. Completely immune to chloride stress corrosion cracking, its hermetic magnetic drive eliminates acid leaks, delivering verified >20,000 hours continuous operation.
How does a JONSN anodizing acid circulation pump maintain continuous operation under -5°C to 5°C sulfuric acid baths?
Hard anodizing operates in 15%–20% sulfuric acid at -5°C to 5°C, where fluid viscosity increases significantly and attacks standard pump metals. A JONSN anodizing acid circulation pump (MRA/MRB series in 316L or Hastelloy C-276) utilizes positive displacement multi-tooth PEEK gears. Flow remains constant despite viscosity shifts, while hermetic magnetic coupling prevents sulfuric acid leaks and zero metal ions dissolve into the bath, ensuring optimal oxide film hardness and transparency.